
Introduction to Valve Bags
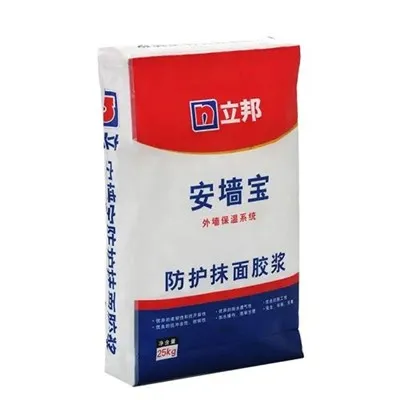
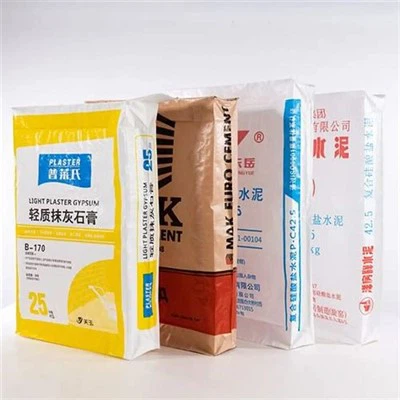
Valve bags are a type of packaging solution widely used in various industries, especially for the packaging of powdered and granular products. These bags are designed with a small opening, or valve, through which the product can be filled. Once filled, the valve self - seals, preventing the product from leaking out and protecting it from external contaminants such as moisture, dust, and pests. Valve bags are commonly made from materials like paper, plastic, or a combination of both, and they offer advantages such as efficient filling, good product protection, and ease of handling. They are used in industries including construction (for cement, sand, and other building materials), food (for flour, sugar, and spices), and chemicals (for fertilizers, pesticides, and industrial powders).
Top 10 Valve Bag Manufacturers
1. Zibo Haosence Packaging Co., Ltd.
Zibo Haosence Packaging Co., Ltd. is a leading player in the valve bag manufacturing industry. The company is committed to providing high - quality packaging solutions that meet the diverse needs of its customers. With years of experience in the field, Zibo Haosence has developed advanced production techniques and a strict quality control system.
The company's valve bags are known for their durability and reliability. They are designed to withstand the rigors of transportation and storage, ensuring that the packaged products remain intact. Zibo Haosence offers a wide range of valve bags, including those made from different materials such as kraft paper, polyethylene, and composite materials. This allows customers to choose the most suitable bag for their specific products.
Features in Valve Bag Production:
- Customization: Zibo Haosence can customize valve bags according to the customer's requirements. This includes different sizes, shapes, colors, and printing options. For example, if a customer needs a valve bag with a specific logo or product information printed on it, the company can easily accommodate such requests.
- High - Quality Materials: The company sources high - quality raw materials for its valve bags. The kraft paper used is strong and has good tear resistance, while the plastic materials are of high - grade quality, providing excellent moisture and chemical resistance.
- Efficient Filling Design: The valve design of their bags is optimized for efficient filling. The self - sealing mechanism ensures that the filling process is fast and accurate, reducing the risk of product spillage.
Advantages:
- Cost - Effective: Zibo Haosence offers competitive pricing for its valve bags. By optimizing its production processes and supply chain management, the company can keep the costs down without compromising on quality.
- Excellent Customer Service: The company has a dedicated customer service team that is available to assist customers throughout the purchasing process. From product咨询 to after - sales support, the team ensures that customers have a smooth and satisfactory experience.
- Global Reach: Zibo Haosence has established a wide distribution network, allowing it to serve customers around the world. Whether it is a small - scale local business or a large multinational corporation, the company can provide timely and reliable delivery of valve bags.
Website: https://www.bulkbaghs.com/
2. Mondi Group
Mondi Group is a global packaging and paper group with a strong presence in the valve bag market. Headquartered in Vienna, Austria, the company operates in more than 30 countries and has a workforce of over 25,000 employees. Mondi has a long - standing reputation for innovation and sustainability in the packaging industry.
Mondi's valve bags are used in a wide range of industries, including agriculture, construction, and chemicals. The company offers a comprehensive portfolio of valve bag solutions, from standard paper valve bags to high - performance plastic and composite valve bags.
Features in Valve Bag Production:
- Sustainable Solutions: Mondi is committed to sustainability and offers valve bags made from renewable and recyclable materials. For example, their paper valve bags are often sourced from sustainably managed forests, and they are working on developing more eco - friendly plastic alternatives.
- Advanced Printing Technology: The company uses state - of - the - art printing technology to create high - quality graphics on its valve bags. This not only enhances the brand image of the customer's products but also provides important product information such as usage instructions and safety warnings.
- Strong Barrier Properties: Mondi's valve bags are designed to provide excellent barrier properties against moisture, oxygen, and other contaminants. This helps to extend the shelf life of the packaged products, especially for sensitive items such as food and chemicals.
Advantages:
- Research and Development Capabilities: Mondi invests heavily in research and development to continuously improve its valve bag products. The company's R & D team is constantly exploring new materials, designs, and manufacturing processes to meet the evolving needs of the market.
- Global Manufacturing Network: With manufacturing facilities located around the world, Mondi can ensure local production and supply for its customers. This reduces transportation costs and lead times, making it more convenient for customers to get their valve bags in a timely manner.
- Industry Expertise: Having been in the packaging industry for many years, Mondi has in - depth knowledge and expertise in valve bag production. The company can provide valuable advice and solutions to customers based on their specific industry requirements.
3. Smurfit Kappa
Smurfit Kappa is one of the leading providers of paper - based packaging solutions globally. The company has a strong focus on innovation, sustainability, and customer service. With operations in over 30 countries, Smurfit Kappa serves a wide range of industries, including food, beverage, and industrial goods.
In the valve bag segment, Smurfit Kappa offers a variety of paper - based valve bags that are known for their quality and performance. The company's valve bags are designed to be strong, reliable, and environmentally friendly.
Features in Valve Bag Production:
- Innovative Design: Smurfit Kappa is constantly innovating in valve bag design. For example, they have developed valve bags with improved stacking properties, which are more stable during transportation and storage. This reduces the risk of damage to the bags and the products inside.
- Recyclable and Biodegradable Options: The company offers valve bags made from recyclable and biodegradable paper materials. This aligns with the growing demand for sustainable packaging solutions in the market.
- Good Printing Quality: Similar to Mondi, Smurfit Kappa has high - quality printing capabilities. Their valve bags can be printed with detailed graphics and text, helping customers to effectively promote their products.
Advantages:
- Customer - Centric Approach: Smurfit Kappa puts the customer at the center of its business. The company works closely with customers to understand their needs and develop customized valve bag solutions. This includes providing on - site support and technical assistance.
- Sustainable Supply Chain: The company has a well - established sustainable supply chain for its paper materials. It sources wood from responsibly managed forests and has strict environmental standards throughout its production processes.
- Strong Financial Position: Smurfit Kappa's strong financial position allows it to invest in new technologies and expand its production capacity. This ensures that the company can meet the increasing demand for valve bags in the market.
4. Bemis Company, Inc.
Bemis Company, Inc. is a global leader in flexible packaging solutions. The company has a wide range of products, including valve bags for various industries such as food, pharmaceuticals, and industrial chemicals. Bemis is known for its high - quality products and innovative packaging designs.
Features in Valve Bag Production:
- Flexible Packaging Options: Bemis offers valve bags made from flexible plastic materials. These bags are lightweight, yet strong, and can be easily customized in terms of size and shape. They are also suitable for products that require a high level of flexibility in packaging.
- Advanced Sealing Technology: The company uses advanced sealing technology to ensure the integrity of its valve bags. The seals are strong and reliable, preventing product leakage and contamination.
- Food - Grade Materials: For food applications, Bemis uses food - grade plastic materials that meet strict safety and quality standards. This ensures that the packaged food products remain safe and fresh.
Advantages:
- Product Innovation: Bemis has a strong focus on product innovation. The company is constantly developing new materials and designs for its valve bags to meet the changing needs of the market. For example, it has introduced valve bags with improved oxygen barrier properties for food products.
- Global Distribution Network: With a global distribution network, Bemis can quickly deliver its valve bags to customers around the world. This is especially important for industries with high - volume and time - sensitive requirements.
- Technical Support: Bemis provides comprehensive technical support to its customers. The company's technical experts can assist customers in choosing the right valve bag for their products and provide advice on packaging processes.
5. ProAmpac
ProAmpac is a leading global flexible packaging company that offers a wide range of packaging solutions, including valve bags. The company has a strong commitment to sustainability and innovation, and it serves customers in various industries such as food, pet food, and consumer goods.
Features in Valve Bag Production:
- Sustainable Packaging Solutions: ProAmpac offers valve bags made from recyclable and compostable materials. The company is actively involved in developing new sustainable packaging technologies to reduce its environmental impact.
- High - Performance Films: The valve bags produced by ProAmpac are often made from high - performance films. These films provide excellent barrier properties against moisture, oxygen, and light, which helps to preserve the quality of the packaged products.
- Customizable Packaging: ProAmpac can customize valve bags according to the customer's specific requirements. This includes different film thicknesses, printing options, and valve designs.
Advantages:
- Innovation - Driven Culture: The company has an innovation - driven culture, which encourages its employees to come up with new ideas and solutions. This has led to the development of several unique valve bag products in the market.
- Customer - Focused Service: ProAmpac places a high emphasis on customer service. The company works closely with customers to understand their needs and provides them with personalized packaging solutions.
- Global Manufacturing and Distribution: ProAmpac has manufacturing facilities and distribution centers around the world, allowing it to serve customers efficiently and effectively.
6. Uflex Limited
Uflex Limited is an Indian multinational flexible packaging company. It is one of the largest flexible packaging companies in the world and has a significant presence in the valve bag market. The company offers a wide range of valve bags for industries such as food, agriculture, and chemicals.
Features in Valve Bag Production:
- Diverse Material Options: Uflex offers valve bags made from a variety of materials, including paper, plastic, and laminates. This allows customers to choose the most suitable material based on the nature of their products.
- Localized Production: The company has manufacturing facilities in different regions, which enables it to provide localized production and support to its customers. This reduces transportation costs and lead times.
- Quality Control: Uflex has a strict quality control system in place. Each valve bag undergoes multiple quality checks during the production process to ensure that it meets the highest standards.
Advantages:
- Cost - Competitiveness: Due to its large - scale production and efficient operations, Uflex can offer valve bags at competitive prices. This makes it an attractive option for cost - conscious customers.
- Technological Expertise: The company has a strong technological base and is constantly investing in new technologies and equipment. This allows it to produce high - quality valve bags with advanced features.
- Cultural Understanding: With its roots in India, Uflex has a good understanding of the cultural and business practices in different regions. This helps the company to better serve its international customers.
7. Huhtamaki Oyj
Huhtamaki Oyj is a global packaging company that specializes in consumer and industrial packaging solutions. The company has a long history of providing high - quality packaging products, including valve bags. Huhtamaki's valve bags are used in industries such as food, chemicals, and building materials.
Features in Valve Bag Production:
- Consumer - Oriented Design: Huhtamaki focuses on consumer - oriented design for its valve bags. The bags are designed to be easy to handle, open, and close, which enhances the user experience.
- Sustainable Initiatives: The company is committed to sustainability and offers valve bags made from renewable and recyclable materials. It also has initiatives to reduce its carbon footprint throughout the production process.
- Product Safety: Huhtamaki places a high priority on product safety. Its valve bags are designed to meet strict safety standards, especially for food and pharmaceutical applications.
Advantages:
- Brand Reputation: Huhtamaki has a strong brand reputation in the packaging industry. Customers trust the company's products for their quality and reliability.
- Research and Development: The company invests in research and development to continuously improve its valve bag products. This includes developing new materials and packaging concepts.
- Global Presence: With a global presence, Huhtamaki can serve customers in different parts of the world. It has local sales and support teams in various countries, which helps to provide better customer service.
8. Sealed Air Corporation
Sealed Air Corporation is a global leader in protective packaging solutions. The company offers a range of valve bags that are designed to provide excellent protection for products during transportation and storage. Sealed Air's valve bags are used in industries such as electronics, automotive, and consumer goods.
Features in Valve Bag Production:
- Shock - Absorbing Properties: The valve bags produced by Sealed Air often have shock - absorbing properties. This is achieved through the use of special materials or internal structures, which help to protect fragile products from damage.
- Anti - Static Features: For electronic products, Sealed Air's valve bags can be designed with anti - static features. This prevents static electricity from damaging the sensitive electronic components.
- Custom - Engineered Solutions: The company can custom - engineer valve bags according to the specific requirements of the customer. This includes designing bags for unique product shapes and sizes.
Advantages:
- Expertise in Protection: Sealed Air has extensive expertise in protective packaging. This allows it to develop valve bags that provide the highest level of protection for different types of products.
- Global Technical Support: The company offers global technical support to its customers. Its technical experts can provide on - site assistance and advice on packaging solutions.
- Continuous Innovation: Sealed Air is constantly innovating in the field of protective packaging. It is always looking for new ways to improve the performance of its valve bags.
9. Bischof + Klein SE & Co. KG
Bischof + Klein is a German family - owned company that specializes in flexible packaging solutions. The company has a long - standing tradition of quality and innovation in the packaging industry, and its valve bags are well - known for their high quality.
Features in Valve Bag Production:
- German Engineering Precision: The valve bags from Bischof + Klein are manufactured with German engineering precision. This ensures that the bags have consistent quality and performance.
- High - Quality Printing: The company offers high - quality printing on its valve bags. The prints are sharp, durable, and can withstand various environmental conditions.
- Wide Range of Applications: Bischof + Klein's valve bags are suitable for a wide range of applications, including food, chemicals, and industrial products.
Advantages:
- Quality - Driven Culture: The company has a quality - driven culture, and every aspect of its production process is focused on delivering high - quality valve bags.
- Long - Term Customer Relationships: Bischof + Klein has built long - term relationships with its customers. The company values customer loyalty and provides excellent after - sales service.
- Industry Leadership: As an industry leader in Germany, Bischof + Klein has access to the latest technologies and industry trends. This allows it to stay ahead of the competition in the valve bag market.
10. Constantia Flexibles Group GmbH
Constantia Flexibles Group GmbH is a leading international manufacturer of flexible packaging solutions. The company offers a variety of valve bags for industries such as food, cosmetics, and pharmaceuticals. Constantia Flexibles is known for its high - quality products and innovative packaging designs.
Features in Valve Bag Production:
- Barrier Technology: The valve bags produced by Constantia Flexibles are equipped with advanced barrier technology. This provides excellent protection against moisture, oxygen, and other contaminants, ensuring the quality and freshness of the packaged products.
- Aesthetic Design: The company focuses on aesthetic design for its valve bags. The bags can be customized with attractive colors and graphics, which helps to enhance the brand image of the customer's products.
- Regulatory Compliance: Constantia Flexibles ensures that its valve bags comply with all relevant regulatory requirements, especially for industries such as food and pharmaceuticals.
Advantages:
- Innovation and Design Capabilities: The company has strong innovation and design capabilities. It is constantly developing new packaging concepts and designs to meet the changing needs of the market.
- Global Production Network: Constantia Flexibles has a global production network, which allows it to serve customers around the world. The company can ensure local production and supply, reducing lead times and costs.
- Customer - Oriented Approach: The company takes a customer - oriented approach, working closely with customers to understand their needs and provide customized valve bag solutions.
Conclusion
The valve bag manufacturing industry is highly competitive, with these top 10 manufacturers leading the way in terms of quality, innovation, and sustainability. Each of these companies has its own unique features and advantages, whether it is Zibo Haosence Packaging Co., Ltd.'s cost - effective and customizable solutions, Mondi Group's focus on sustainability and global reach, or Smurfit Kappa's customer - centric approach.
As the demand for valve bags continues to grow in various industries, these manufacturers are likely to play a crucial role in meeting the needs of customers around the world. They will need to continue investing in research and development, improving their production processes, and enhancing their customer service to stay competitive in the market. Additionally, with the increasing emphasis on environmental protection, the industry will also see more efforts towards developing sustainable valve bag solutions in the future.